Carton Print Inspection: How the Process Works
Follow the operating sequence for carton print inspection, from preparing the input and controlling the main task to handling exceptions and checking results.
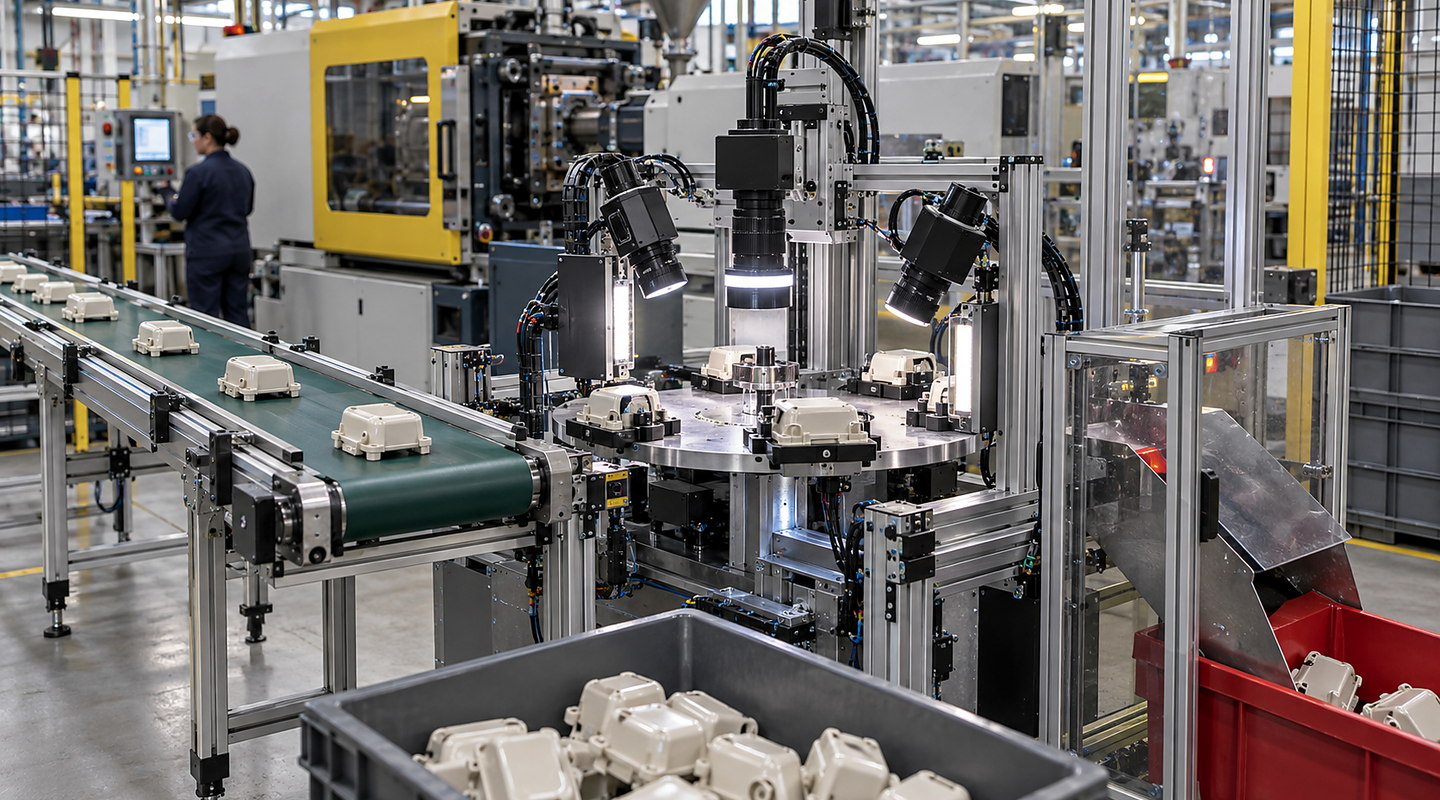
Photographs illustrate general machine-vision inspection. Carton print checks must be trialled with the actual artwork, variable data and line presentation.
Carton Print Inspection should be considered as part of a complete production sequence: inputs are prepared, the main task is controlled, exceptions are handled and results are checked.
For your application, the important details include visible defect or measurement definition for carton artwork & variable-print checks, good, bad and marginal sample range, part presentation and production speed, and optics, lighting and environmental conditions.
Understand the complete route from input to accepted output — Carton Print Inspection
Plan carton print inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Follow the material or part through each operating step and include recovery, cleaning and change in the real cycle.
Discuss your application

From an approved carton design to a controlled print decision
Carton inspection works best when artwork identity, variable text and physical print defects have separate acceptance rules. A readable date can still be the wrong date, and the correct artwork can still have missing print. Define those outcomes before choosing a camera or software tool.
Choose the correct reference for each field
Use the approved artwork revision for fixed logos, language panels and product identity. Use the production job or authorised batch record for changing dates and lot text. OCR reads characters; verification then compares the result with the permitted value or rule. A camera reading the same incorrect value that the printer received is not an independent check unless the expected data source is also controlled.
Separate print quality from carton movement
Include carton skew, flap position, creases, glossy varnish and normal supplier variation in trials. First locate the panel to inspect, then judge the required feature within it. Otherwise a moving panel edge may look like missing ink. Agree which folded or hidden panels cannot be assessed at the proposed station and whether another view is required.
Test near matches, not only blank print
Prepare approved examples of the wrong product variant, old artwork revision, transposed digits, incomplete characters and a correct but faint code. For medical-carton work, let the responsible quality team define critical content and release requirements; this optical check does not itself establish regulatory compliance. Keep borderline accepted cartons as well as obvious rejects so the trial measures unnecessary rejection separately from missed faults.
Carry the result through to the correct carton
Record artwork/recipe identity with the image decision and define what happens when the image, expected text or result is unavailable. Challenge a carton removed between camera and reject, consecutive rejected cartons and a restart with cartons still on the conveyor. A reject signal alone does not demonstrate that the intended pack was removed.
Decide what the production record must explain
A useful exception record identifies the job, inspection recipe, failed field and retained evidence, subject to the agreed retention policy. Review changed artwork before production resumes rather than silently widening a threshold to accept it. Use the specification checklist to agree responsibility for expected text, reference images and challenge samples.
Keep connected responsibilities clear
Your final carton print inspection scope must also account for recipe, reject and line-control interfaces, false-accept, false-reject and challenge criteria, current regulations and the conditions at your site.
- A camera can only assess a property made visible and repeatable by the inspection setup.
- Sample diversity and marginal cases determine how meaningful a feasibility result is.
- Visual inspection does not replace hidden, destructive, functional or statutory tests.